



The CORYNESIS™ Fermentation Process
CORYNESIS™ TECHNOLOGY How CORYNESIS Technology Produces Free L-Amino Acids CORYNESIS™ is the fermentation technology behind the FERMATIVE range, built on Corynebacterium glutamicum, a naturally occurring soil bacterium with a well-established role in amino acid biosynthesis, and developed through continuous research to produce a targeted amino acid profile with stable, replicable results at industrial scale. What […]


CORYNESIS™ TECHNOLOGY
How CORYNESIS Technology Produces Free L-Amino Acids
CORYNESIS™ is the fermentation technology behind the FERMATIVE range, built on Corynebacterium glutamicum, a naturally occurring soil bacterium with a well-established role in amino acid biosynthesis, and developed through continuous research to produce a targeted amino acid profile with stable, replicable results at industrial scale.
What distinguishes a precision fermentation product from a conventional amino acid solution is its biological complexity. The fermentation process does not produce a single compound in isolation. It generates a complex matrix of hundreds of metabolites working in concert, including free amino acids, organic acids, vitamins, phenolic compounds, and signalling molecules, each produced by the organism’s own metabolism. This biological complexity defines the agronomic character of the final product. This page explains how CORYNESIS Technology produces that complexity and what it delivers to the crop.
The Production Organism
Corynebacterium glutamicum is a gram-positive, non-pathogenic soil bacterium first isolated in Japan in 1957 for its natural ability to secrete L-glutamic acid under specific growth conditions. It is aerobic, poses no known risk to humans, animals, or the environment, and grows robustly under industrial fermentation conditions. Its central metabolic network, connecting glycolysis, the pentose phosphate pathway, and a complete TCA cycle, links directly to the biosynthetic pathways for all major amino acids.
Production uses C. glutamicum strains selected for a consistent amino acid profile and verified for stability before each production campaign.
The Fermentation Process
CORYNESIS fermentation takes place in stirred-tank bioreactors under aerobic conditions. Using glucose as the carbon source and ammonium as the nitrogen source, C. glutamicum builds free L-amino acids from these simple inputs, accumulating them in the broth alongside a spectrum of biologically active compounds produced by microbial metabolism.
Inoculum Preparation
Every production run begins with a carefully prepared inoculum, the starter culture that is transferred into the main fermentation vessel. Inoculum quality is one of the most critical determinants of fermentation performance: an inoculum that is not in the right physiological state, or that has been compromised by contamination or genetic drift, will underperform regardless of how well the rest of the process is controlled.
The inoculum is developed through a seed train, a series of progressively larger culture vessels from laboratory flask to seed fermenter, each stage running under controlled conditions until the culture reaches the target cell density and metabolic activity. Stability and productive capacity are verified at each stage before transfer. Continuous sterilisation keeps the seed culture and main vessel free of contaminating organisms at every stage.
Medium Composition
The fermentation medium is a precisely formulated aqueous solution that provides everything the production organism requires. All components are defined and controlled from batch to batch, so consistent inputs give a consistent amino acid profile.
| Carbon source | Glucose, principally derived from starch hydrolysis of corn, cassava, or similar crops, serves as the main carbon and energy source. It provides the carbon skeletons that form the backbone of every amino acid biosynthesised during the run. |
|---|---|
| Nitrogen source | Ammonium sulfate and ammonia gas are the principal nitrogen inputs. The bacteria assimilate ammonium ions through enzymatic reactions and incorporate the resulting amino groups into glutamate, from which nitrogen is distributed to all other amino acids via transamination. |
| Vitamins | Biotin and thiamine are essential cofactors for C. glutamicum metabolism. Biotin in particular plays a regulatory role in glutamate secretion, and its concentration in the medium directly influences the membrane conditions that trigger amino acid export from the cell. Both are supplied at concentrations calibrated for the target amino acid profile. |
| Minerals & trace elements | Potassium phosphate, magnesium sulfate, iron sulfate, manganese sulfate, and a range of trace elements at micro- to millimolar concentrations support enzyme function, cell membrane integrity, and the redox reactions involved in amino acid biosynthesis. Their concentrations are defined and controlled to avoid both deficiency and toxicity effects on the production strain. |
| Other additives |
Small amounts of soybean protein hydrolysate or yeast extract provide additional growth factors and trace organic nutrients that support strain performance. Food-grade antifoam agents are also used as needed to manage foam generated by agitation and aeration. |
| Ammonia gas | Supplied continuously throughout the run for dual purpose: as the primary nitrogen donor for amino acid biosynthesis, and as the alkalising agent that neutralises organic acids produced as metabolic by-products, maintaining the culture pH within the optimal range. |
Fed-Batch Operation
CORYNESIS fermentation runs in fed-batch mode, the established standard for amino acid production at industrial scale. This configuration is specifically chosen because it delivers higher yield, higher productivity, and greater process reproducibility than simpler batch approaches, while maintaining the precise control needed to achieve a consistent targeted amino acid profile batch after batch.
Process Control
Throughout the fed-batch run, key process parameters are continuously monitored and actively controlled. Each parameter is critical to achieving the target amino acid profile and maintaining fermentation performance:
| pH | Culture pH is maintained within a defined range by automatic addition of ammonia, which simultaneously serves as the nitrogen source for amino acid biosynthesis and as the alkalising agent that neutralises the organic acids produced as metabolic by-products. This dual role means ammonia is consumed continuously throughout the run. |
|---|---|
| Aeration & oxygen transfer (OTR) | Aerobic conditions must be maintained without interruption. The OTR into the broth is actively managed through agitation speed and airflow rate. The optimal OTR differs between amino acids, as different biosynthetic pathways carry different oxygen demands, and the process is configured for the conditions that favour the target amino acid composition. |
| Temperature | Temperature is held within the optimal range for C. glutamicum activity and is chosen to suit the target compounds. It affects not only growth rate and enzyme kinetics but also the balance between metabolic pathways, so temperature is one of the levers that shape the final amino acid composition. |
| Carbon feed rate |
The rate at which glucose is fed into the vessel is the central control variable of the fed-batch process. It determines carbon availability, growth rate, oxygen demand, and the rate of amino acid production simultaneously. The feed profile is set to match the target amino acid composition of the FERMATIVE range and is one of the key parameters that define the character of the final product. |
Downstream Processing
At the end of the fed-batch production phase, the harvested broth is processed using a deliberately minimal sequence of operations. Rather than intensive purification that would strip away biologically active compounds, the process is designed to preserve the full complexity of the fermentation output while delivering a clean, stable, and homogeneous liquid product.
Broth HarvestFed-batch run completed; full broth contents collected from the bioreactor.
Dilution & HomogenisationBroth diluted with water to the target concentration and mixed until all components are evenly distributed.
FiltrationFiltered to remove particulate matter and achieve product clarity.
Quality CheckAmino acid profile, total nitrogen, pH, and physical parameters verified.
PackingFilled into final product containers; labelled and released for distribution.
The finished liquid may contain fine submicron biological particles, which settle gradually on standing. Shaking before use redistributes any settled material uniformly.
The Final Product
Free L-Amino Acids
The dominant amino acids in the CORYNESIS Technology product are L-glutamic acid, L-alanine, and L-proline, each with a distinct agronomic role:
| L-Glutamic acid | The central hub of nitrogen metabolism in plants. Once absorbed, glutamic acid serves as the primary nitrogen donor in transamination reactions, fuelling the biosynthesis of all other amino acids and nucleotides the plant requires. Research suggests it may also interact with glutamate receptor-like (GLR) channels, with implications for root development and calcium signalling, making it both a nitrogen source and a signalling molecule in the rhizosphere. |
|---|---|
| L-Alanine | A simple, rapidly metabolised amino acid that contributes directly to energy metabolism and participates in the plant response to low-oxygen conditions. Its rapid assimilation makes it one of the most readily available nitrogen forms in the product. |
| L-Proline | Proline accumulates naturally in plants under drought, salinity, and temperature stress, functioning as a compatible solute that stabilises membrane integrity, protects enzyme structure, and scavenges reactive oxygen species. Exogenous proline application pre-conditions plants against abiotic stress, improving recovery and maintaining productivity under adverse conditions. |
| Residual ammoniacal nitrogen |
This fraction is an immediately plant-available inorganic nitrogen source that complements the organic amino acid nitrogen, giving the product two forms of nitrogen. |
The Biological Matrix
Alongside the amino acid fraction, microbial metabolism generates a broad range of additional bioactive compounds that contribute independently and collectively to the product’s agronomic activity. Metabolomics profiling of the product has identified phenolic compounds, diverse carboxylic acids, B-group vitamins and signalling metabolites.
| B-group vitamins | Biotin, thiamine (B1), and pantothenic acid (B5) are present in the fermentation broth as residual cofactors from the production medium and as metabolic products of the organism itself. These vitamins participate in plant enzyme systems, support root growth, and enhance the activity of soil microorganisms, contributing to both direct crop nutrition and rhizosphere biology. |
|---|---|
| Organic acids | Short-chain organic acids, including citric, succinic, pyruvic, and lactic acids, are natural metabolic by-products of the TCA cycle activity that drives amino acid biosynthesis. In the soil environment, these acids chelate mineral micronutrients, increasing their solubility and bioavailability to plants, and serve as readily metabolisable carbon substrates for beneficial soil microbial communities. |
| Phenolic compounds | Fermentation transforms phenolic compounds naturally present in the plant-based medium inputs, particularly soybean hydrolysate and corn-derived materials. Research has confirmed that C. glutamicum fermentation of plant biomass substrates produces broths with elevated phenolic and flavonoid content compared to unfermented substrates. These compounds act as antioxidants in the rhizosphere and have demonstrated biostimulant activity in crops, including enhancement of germination, root development, and resistance to oxidative stress. |
| Microbial metabolites & short peptides | The minimally processed broth retains short-chain peptides, nucleotides, and cell wall-derived compounds produced during microbial metabolism. Short peptides are absorbed by plant roots via dedicated peptide transporter systems and serve as both nitrogen sources and signalling molecules that modulate root architecture and plant defence responses. |
Quality Verification
Every production batch is verified against a defined set of analytical parameters before release. Quality control spans the full production process, from raw material assessment through fermentation monitoring to finished product analysis.
| Parameter | What It Confirms |
|---|---|
| Amino acid profile (aminogram) | Free L-amino acid composition matches the target profile; dominant peaks at glutamic acid, alanine, and proline verified by HPLC. |
| Total nitrogen | Organic nitrogen (from amino acids) and ammoniacal nitrogen quantified and declared separately. |
| Metabolomics profiling | Identifies and maps the full spectrum of metabolites in the product, including phenolic compounds, carboxylic acids, vitamins, and signalling metabolites, confirming biological complexity and batch consistency. |
| pH | Product stability and compatibility with application equipment and tank mixes confirmed. |
| Physical appearance | Colour, clarity, and sediment level consistent with batch specification; minimal natural sediment is acceptable and expected. |
| Microbial safety | Absence of pathogenic organisms confirmed before release. |
| Heavy metals | Lead, cadmium, arsenic, and mercury within regulatory limits for agricultural inputs. |

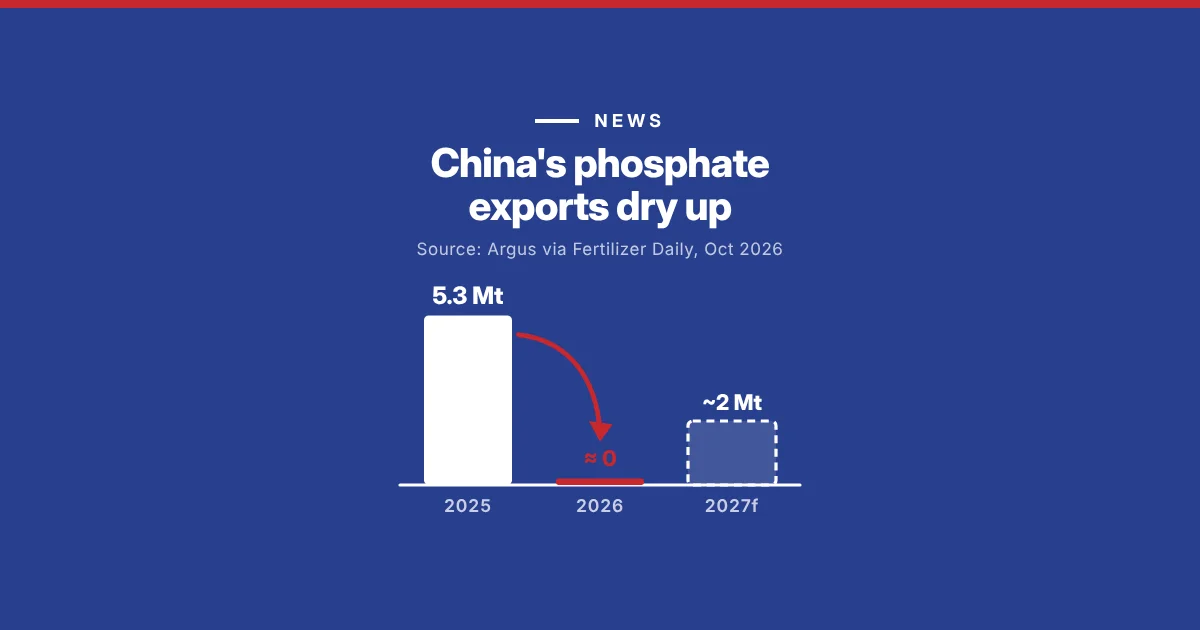
China, which exported about 5.3 million tonnes of phosphate fertilizer in 2025, has shipped almost none in 2026. With sulfur scarce and phosphate prices high, import-dependent markets face a tight season, and every kilo of phosphorus needs to work harder. At Van Polder, we believe a tight phosphate market is a reason to look again […]
If you are starting a banana farm, Panama disease (Fusarium wilt of banana) is the risk to plan for. How to prevent Panama disease in bananas comes down to keeping the fungus out, because no fertilizer prevents or cures it and once it is in the soil it stays for decades (Pegg et al., 2019; […]
A government project in Bangladesh’s Rajshahi Division has brought solar-powered pumps, including solar drip systems for orchards, to drought-prone land where groundwater has been falling for decades. The Prime Minister wants all diesel irrigation pumps converted to solar within five years. For growers who move to drip, the next step is to feed the crop […]
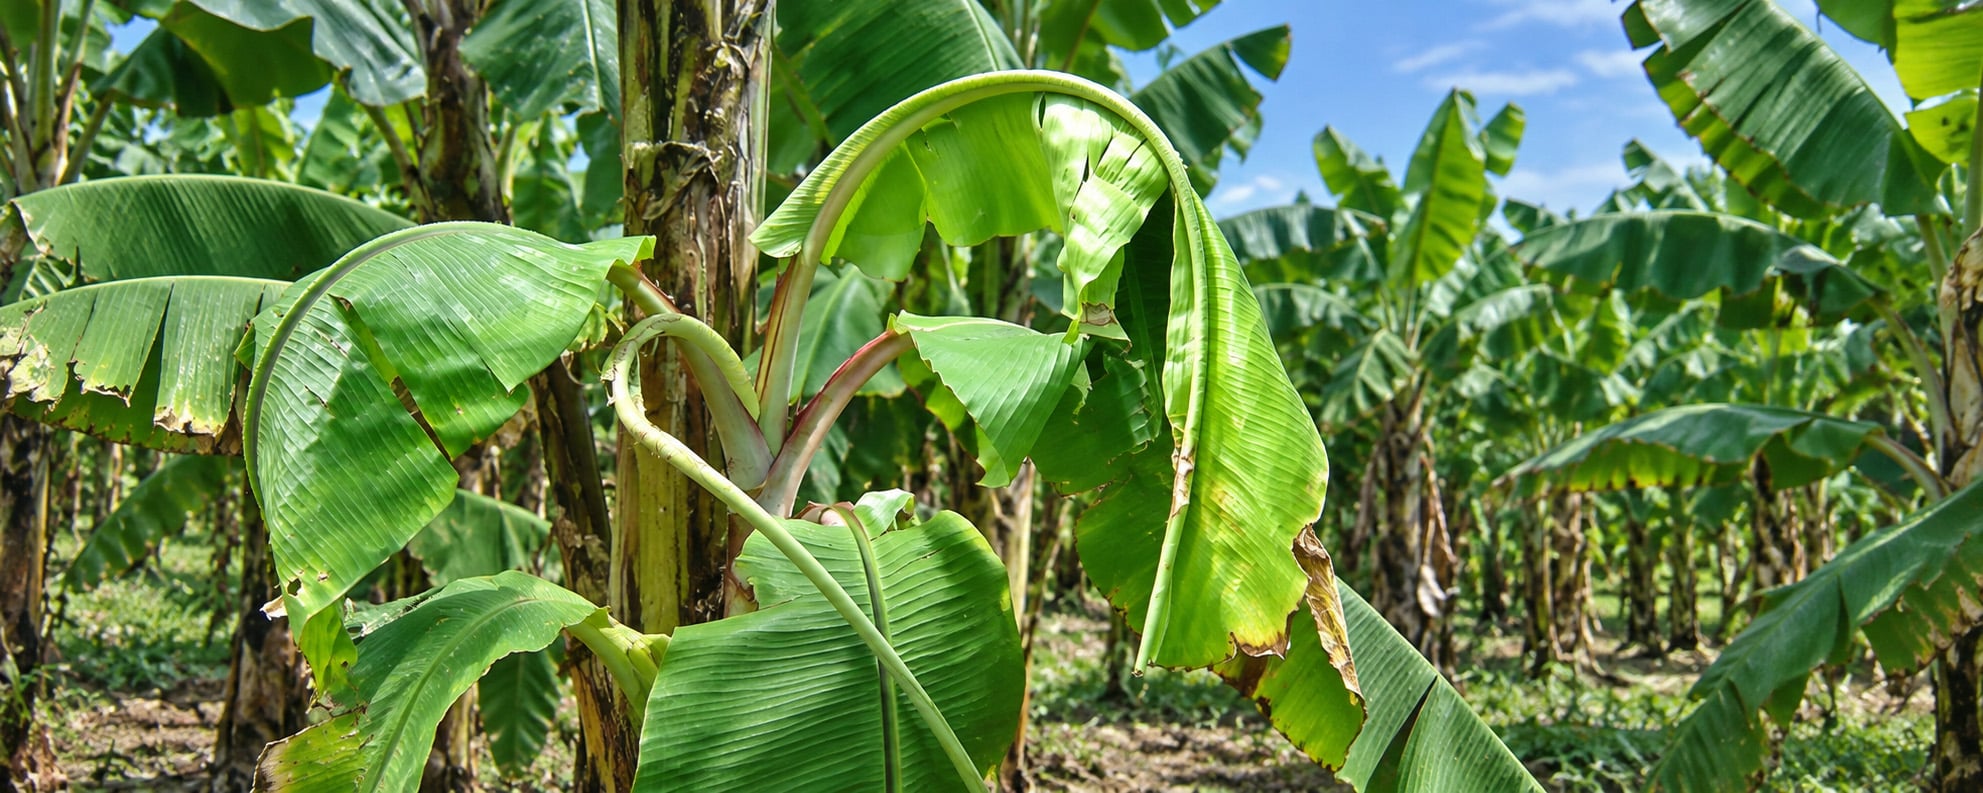
Calcium deficiency in banana shows first on the youngest leaves, as thickened veins and a saw-tooth pattern of yellow and dead tissue along the leaf margin, and in severe cases as “spike leaf”, new leaves with little or no blade, and poor-quality fruit (Turner, 1987; Martin-Prével, 1980). On most plantation soils it is not a […]
A calcium fertilizer supplies the calcium that holds plant cell walls and membranes together, but whether it reaches the fruit depends as much on water flow as on the fertilizer you choose. Calcium travels with water to the leaves and barely moves out of them again, so fruit and young leaves can run short even […]
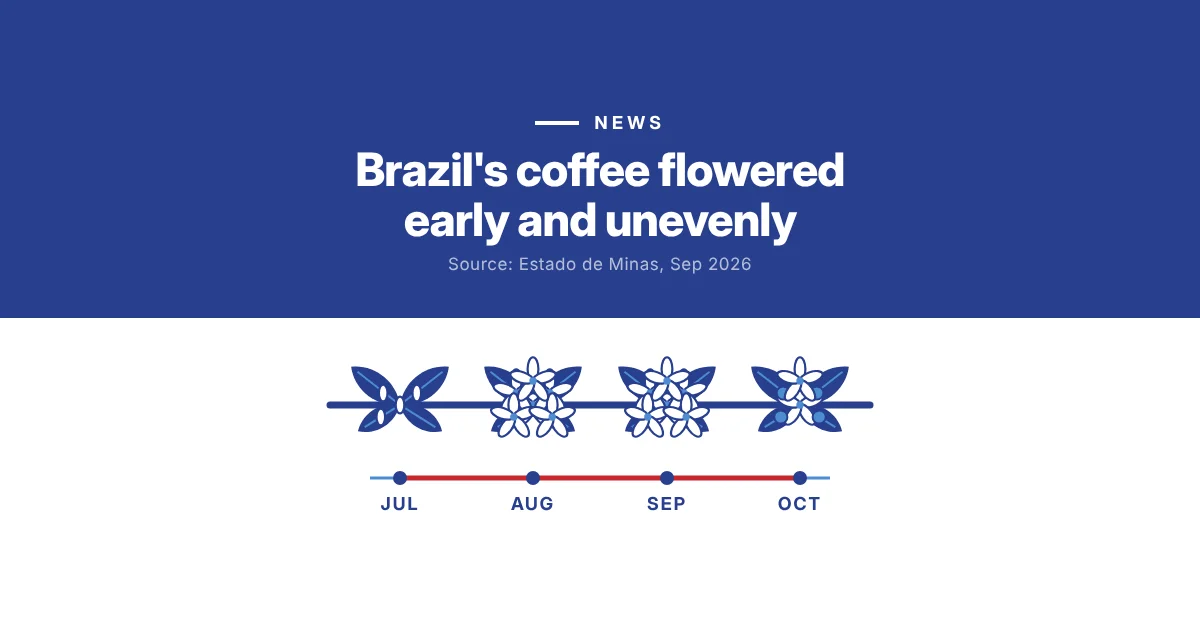
An unusually wet winter brought coffee flowering in Minas Gerais forward by about a month, in several separate waves. With October forecast to be hotter than normal and rain patchy, the question for 2027 is now how many of those flowers turn into fruit. At Van Polder, we believe a strong flowering is only the […]